 Q2
 QIDI Box
 Plus 4
 Q1 Pro
 X-Max 3


How to Dry Filament for 3D Printing

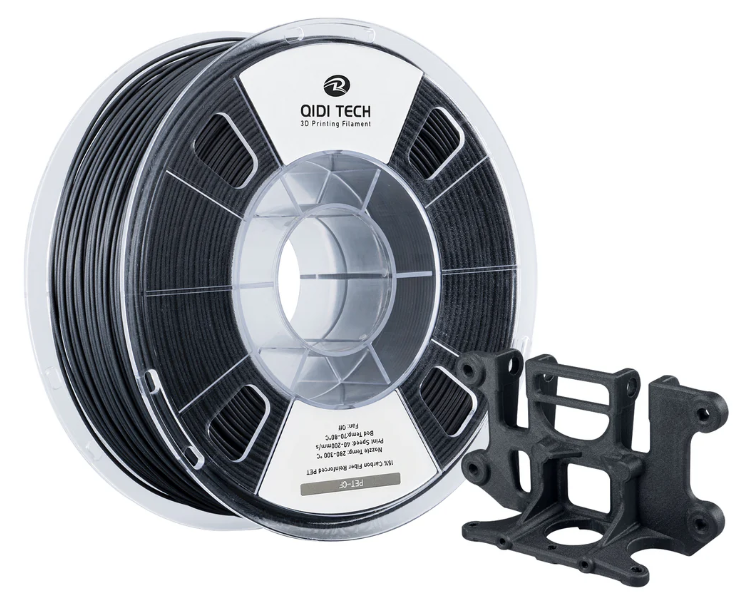
To dry filament, hold it at a temperature below its glass transition point for four to six hours in a filament dryer, blast oven or food dehydrator, then keep it sealed with desiccant. PLA dries at 45-55 °C, PETG at 55-65 °C, ABS and ASA at 60-70 °C, TPU at 40-50 °C, and nylon or carbon-fibre nylon at 80-100 °C. Never exceed the material's softening point, or the spool deforms.
3D printing with damp filament can result in a number of issues, from poor-quality prints to even possible damage to the printer. Most filaments have a tendency to absorb moisture from the air, and that tends to affect their performance when printing. You may notice strange blobs, too much stringing, or weak layer adhesion in your prints. These issues can turn what should be a relatively easy project into a frustrating experience. Fortunately, there are efficient ways to dry filament and bring about an improved printing result. This guide covers the temperatures, the times, the equipment, and the storage limits that keep the material dry once you have done the work.
Filament Drying Temperature and Time Chart
This is the reference most people come here for. The QIDI-published column is taken from QIDI's own technical data sheets for those specific filaments; the general column is the safe consumer-dryer window for the material class.
| Material | Drying temperature | Drying time | Hard ceiling | Storage target |
|---|---|---|---|---|
| PLA | 45-55 °C | 4-6 h | 55 °C | < 20% RH |
| PLA-CF (QIDI spec) | 50 °C | 4-6 h | 55 °C | < 20% RH |
| PETG (QIDI spec) | 55-65 °C | 4-6 h | 70 °C | < 20% RH |
| ABS / ASA | 60-70 °C | 4-6 h | 80 °C | < 20% RH |
| TPU | 40-50 °C | 4-6 h | 55 °C | < 20% RH |
| PC | 70-80 °C | 6-8 h | 90 °C | < 15% RH |
| PA / nylon in a consumer dryer | 70-80 °C | 8-12 h | 90 °C | < 15% RH |
| QIDI UltraPA and UltraPA-CF25 (QIDI spec) | 80-100 °C | 4-6 h | 110 °C | < 15% RH |
| QIDI PET-CF (QIDI spec) | 100 °C | 4-8 h | 110 °C | < 15% RH |
| QIDI PPS-CF (QIDI spec) | 100-140 °C | 8-12 h | 160 °C | < 20% RH |
Two practical notes follow from that chart. First, most consumer filament dryers stop at 60-70 °C, so anything in the bottom three rows needs a blast drying oven rather than a desktop unit. Second, the hard-ceiling column exists because the spool melts before the filament does: above roughly 160 °C even a PPS-CF spool starts to deform, and a PLA spool sags well below 70 °C.
What Is the Maximum Drying Temperature for PLA?
Keep PLA at or below 55 °C. PLA's glass transition sits around 60-65 °C, and once the polymer passes that point the coils on the spool soften enough to weld to each other. The result is a spool that unwinds in fused clumps, which is a much harder problem to fix than the moisture you were trying to remove. A 50 °C setting for six hours removes essentially all the absorbed water in a 1 kg PLA spool with a comfortable margin. If your dryer only offers preset material profiles, use the PLA preset and add time rather than heat.
The Importance of Dry Filament in 3D Printing
Moisture: The Enemy of Print Quality
Wet filament can cause a lot of problems in 3D printing. When this filament heats up, the moisture inside it turns into steam, leading to symptoms like bubbles in the printed plastic, inconsistent extrusion, and sometimes even popping noises during printing. The effect is not only cosmetic: published work on moisture sorption and degradation of polymer filaments used in 3D printing documents measurable loss of mechanical performance once filaments take on water.

Why Filaments Become Damp
The fact is that most 3D printing materials absorb moisture from the air over time as the water molecules get between the polymer chains in the filament. Different materials absorb moisture at different rates depending on their material type and the humidity around them.
4 Key Signs of Wet Filament
You can often spot a wet filament before printing:
- Dull Appearance: Wet filament might look less shiny than dry filament.
- Increased Brittleness: Moist filament tends to break more easily.
- Print Defects: Excessive stringing, poor layer adhesion, or bubbly prints can indicate wet filament.
- Unusual Printing Sounds: You might hear sizzling or popping when printing with wet filament.
Recognizing these signs helps you tackle moisture problems early, potentially saving time and materials in your 3D printing work.
Types of Filaments and Their Moisture Sensitivity
Not all 3D printing filaments are equal in how much they react to moisture. Their sensitivity to humidity can be very large; it alters the way you will treat and store them.
QIDI publishes a saturation water-absorption figure on its filament data sheets, which is a more useful ranking than "very hygroscopic" versus "somewhat hygroscopic":
| Filament | Water absorption at saturation | How fast it becomes a problem | Storage requirement on the data sheet |
|---|---|---|---|
| QIDI UltraPA (nylon) | 2.10% | Hours in open air | < 15% RH, sealed with desiccant |
| QIDI UltraPA-CF25 | 1.09% | Hours in open air | < 15% RH, sealed with desiccant |
| QIDI PETG Translucent | 0.06% | Weeks | Sealed with desiccant |
| QIDI PPS-CF | 0.05% | Weeks, but surface water still ruins a print | < 20% RH, sealed with desiccant |
Highly Moisture-Hungry Filaments: Nylon and TPU
Nylon and TPU top the chart on the subject of moisture sensitivity. These filaments can absorb an impressive amount of water within several hours of exposure to humid air.
Nylon is strong and has a tendency to be flexible, but it is also one of the most sensitive materials to moisture. QIDI lists 2.10% saturation water absorption for its UltraPA nylon, which is enough to produce severe print quality issues: bubbling, stringing and weak layer adhesion. Detailed settings for the whole family live in the nylon 3D printing guide.
TPU is also highly hygroscopic. This elastomeric filament can produce prints that display surface imperfections and inconsistent flexibility when damp.
Middle-Ground Materials: PETG and PLA
While more resistant to moisture than nylon or TPU, PETG can still absorb enough water to affect print quality over time. It may show signs of moisture contamination after a few weeks of exposure to humid air.
Often considered one of the easiest filaments to work with, PLA is still somewhat hygroscopic. It absorbs moisture more slowly than PETG, but it can become problematic if stored improperly for extended periods.
Moisture-Resistant Filaments: ABS
ABS is one of the less hygroscopic filaments out there. It absorbs moisture at a way slower rate compared to some other common 3D printing materials. However, that does not make ABS immune: a study of moisture absorption and desorption by ABS filament found the effect on printed parts is real once the material has been left exposed long enough.

Method 1: Using Commercial Filament Dryers
Commercial Filament Dryer Mechanics
Commercial filament dryers use controlled heat and air circulation to remove moisture from 3D printing materials. These devices typically consist of a heating element, a fan for air circulation, and a chamber to hold the filament spool. The heat causes the moisture within the filament to evaporate, while the circulating air carries the moisture away, effectively drying the material.
Choosing Settings
Use the chart at the top of this page. Two rules matter more than the exact number you pick:
- Stay under the hard ceiling for that material. Heat above the ceiling softens the spool, not just the filament.
- When in doubt, add hours rather than degrees. Doubling the time is safe; adding 20 °C is not.
Always check your filament manufacturer's recommendations as well, since optimal settings can vary between brands and specific formulations.
Method 2: Drying Filament in an Oven
Oven Selection
Choose an oven with precise temperature control. Convection ovens work well due to their air circulation. Use a separate oven from food preparation to avoid contamination. Note that many household ovens overshoot their setpoint by 15-25 °C during the heat-up cycle, which is exactly how PLA spools get ruined — put an independent thermometer inside and watch the first cycle.
Drying Process
Preheat the oven to the right temperature for your filament.
- Wrap the filament loosely in parchment paper or place it on a clean tray.
- Put the filament in the oven, ensuring multiple spools don't touch.
- Set a timer based on your filament type.
- Check occasionally to prevent overheating or deformation.
- After drying, let the filament cool slowly in the oven.
- Store the cooled filament in an airtight container with desiccant.
Oven drying is effective but requires careful monitoring. Always follow the manufacturer's guidelines for your specific filament.
Method 3: Drying Filament with a Food Dehydrator
Adapting Your Dehydrator
Remove the food trays from your dehydrator and fill it with filament spool holders. Leave some space between the spools to allow air to flow freely around them for uniform drying. You may want to create custom spool holders for your dehydrator using heat-resistant materials to ensure maximum spacing if necessary.
Setting Temperature and Time
Set the temperature according to the chart above: 45-55 °C for PLA, 55-65 °C for PETG, 40-50 °C for TPU, all for four to six hours. Most food dehydrators top out near 70 °C, which rules them out for nylon, PET-CF and PPS-CF. Start at the low end of the range and add time if the filament is still damp.
Pros and Cons
Among the benefits food dehydrators are that they are low-cost, simple to operate, and ensure mild and uniform heating. However, they have several disadvantages, too. Most models can provide only a limited range of temperatures, which may be inappropriate for all types of filaments. Large spools just won't fit in some dehydrators. In the case of using a dehydrator both for food and filament, there is a risk of cross-contamination.
Method 4: DIY Filament Drying Solutions
Creating a Desiccant Chamber
Create a simple drying chamber from an airtight container. Line the bottom with desiccant beads or packets. Set up a small mesh platform above the desiccant to hold the filament spool. Seal the container and store it in a cool, dry area. This method takes its time but is safe for all filament types.
Using Silica Gel Packets
Place your filament spool in a resealable plastic bag with a number of silica gel packets. Pull out as much air as possible before sealing it. This is ideal for maintaining already dry filament, or when mildly damp filament has absorbed a little moisture. Replace silica gel packets regularly for continued effectiveness or regenerate them.
Building a Heat Box
Prepare a heating box with any low-wattage light bulb or heating pad and a thermometer in a wooden or plastic box. Fasten the heating element at the bottom of the box, provide a small shelf above for holding the filament spool, and closely monitor the temperature to avoid overheating. This gives more control, but it is not a set-and-forget solution.
Method 5: Drying Filament While You Print
Pre-drying solves the moisture that is already in the spool. It does nothing about the water the filament absorbs during a 30-hour nylon job in a humid room. That is the gap active in-print drying closes.
Does the QIDI Box Dry Filament While Printing?
Yes. The QIDI Box holds its sealed chamber at a constant 65 °C throughout the print, so the filament is kept dry from the first layer to the last rather than only at the start. One unit holds four spools, and up to four units can be linked for 16 filaments in a single job. It also reads NFC-tagged QIDI spools to load the right material profile automatically, and its tangle and clog detection pauses the job instead of letting the printer air-print. The full feature walkthrough is in the QIDI Box guide.
Two limits are worth knowing. A 65 °C chamber holds material dry and slowly drives off surface moisture; it is not a substitute for an 80-100 °C blast-oven cycle on a nylon spool that has been sitting open for a month. And 65 °C is above the safe ceiling for nothing in the common range except PLA at the very top end, so QIDI Box drying is comfortable for PETG, ABS, ASA, PA and CF composites alike.
What About Filament Drying on the QIDI Q2?
The Q2 does not dry filament by itself. Its second-generation independent chamber heater reaches 65 °C, but that chamber heats the printed part, not the spool — the spool sits outside it. To dry filament on a Q2, either pre-dry the spool in a dedicated dryer or blast oven, or attach a QIDI Box, which is the accessory that actually holds the spool at 65 °C during the job. The same distinction applies to every QIDI machine with an actively heated chamber: chamber heating controls warping and layer bonding, spool drying is a separate function. If you want the background on what a heated chamber does and does not do, see the temperature-controlled chamber explainer.
Filament Drying Guidelines for Specific 3D Printing Materials
PLA and PLA-CF: Low-Temperature, Short-Duration Drying
Dry PLA at 45-55 °C for 4-6 hours. QIDI's data sheet for PLA-CF specifies 50 °C for 4-6 hours, and that setting works equally well for unfilled PLA. PLA is less sensitive to moisture than nylon, but drying will not hurt it. Do not exceed 55 °C or the coils can fuse. A food dehydrator or low-temperature dryer handles this comfortably.
PETG: Medium-Heat, Moderate-Time Drying
Dry PETG at 55-65 °C for 4-6 hours, the range QIDI publishes for its PETG series. Compared to PLA, PETG absorbs moisture more readily and shows it as stringing first. Keep the setting under 70 °C. A filament dryer or a well-controlled oven both work.
Nylon and Carbon-Fibre Nylon: High-Heat, Blast-Oven Drying
QIDI specifies 80-100 °C for 4-6 hours in a blast drying oven for both UltraPA and UltraPA-CF25, then storage below 15% RH sealed with desiccant. If all you have is a 70 °C consumer dryer, run 70-80 °C for 8-12 hours instead and accept that the result is good rather than perfect. Nylon is the material where drying discipline pays off most: it is the one that absorbs the most water by mass of anything in a typical filament shelf.
Flexible Filaments: Gentle, Prolonged Drying
Dry flexible filaments like TPU at 40-50 °C for 4-6 hours. These materials are moisture-sensitive but deform at higher temperatures. Use lower heat and longer times. A food dehydrator or low-temperature dryer works well.
Three Ways to Determine When Filament is Dry
1. Examine the Filament's Surface
If the filament surface is matte, it is generally a sign of dryness. When the filament is dried properly, it should be even in colour and texture. Inspect the filament for any air bubbles or irregularities, which could indicate that the filament still retains some moisture. At times, visual inspections cannot always be relied upon.
2. Measure Weight Loss
Weigh the filament spool before and after drying. A decrease in weight shows a loss of moisture. For most filaments, a drop in weight by some 0.2 to 0.5% would indicate that the filament has been sufficiently dried. On a 1 kg spool that is 2-5 g, so a kitchen scale reading to 1 g is the minimum useful resolution.
3. Conduct a Test Print
Do a small test print with the newly dried filament. Look for less stringing, fewer surface defects, and better layer adhesion. Compare against a print made before drying. If problems persist, further drying may be necessary — or the problem was never moisture, in which case work through the general troubleshooting guide instead.

Strategies to Prevent Moisture Absorption During Printing
1. Use Filament Dry Boxes for Active Spools
Store your filament in a dry box while printing. These containers maintain low humidity either through desiccants or through active dehumidification. Most dry boxes have a way for the filament to feed directly to the printer, reducing exposure to ambient moisture. On a tight budget, improvise a dry box using an airtight container with a filament feed hole and desiccant packs; a purpose-built filament dry box saves the fabrication step.
2. Control Printing Environment Humidity
Keep the humidity in your printing space to a minimum. A dehumidifier should be able to keep the relative humidity below 50% for most filaments, and sealed storage should sit far lower — below 20% RH for general materials and below 15% RH for nylon and CF composites. You can measure the current level using a hygrometer. Enclosing the printer creates a controlled environment for very moisture-sensitive materials such as nylon or TPU.
3. Perform Regular Maintenance Checks
Check your filament for moisture absorption periodically, mainly by changes in texture, color, and brittleness. Periodically weigh your spools for detected moisture gain. Work out some form of rotation system with your filament stock so you can use the oldest spools before long-term exposure. Refresh desiccants in storage containers periodically, typically every few months or as indicated by color changes.
FAQs About Drying 3D Printer Filament
How long does it take to dry filament?
Four to six hours covers PLA, PLA-CF, PETG, ABS, ASA and TPU, and matches QIDI's published cycle for UltraPA and UltraPA-CF25 in a blast oven. Eight to twelve hours is the figure for PPS-CF, and for nylon dried in a lower-temperature consumer dryer that cannot reach 80 °C. A spool that has been open in a humid workshop for months may need a second cycle.
Can you over-dry filament?
You cannot remove more water than is there, so time is not the risk — temperature is. Holding a spool above its softening point welds neighbouring coils together and warps the spool flanges, and that damage is permanent. Stay under the hard-ceiling column in the chart above and long cycles are harmless.
What humidity should filament be stored at?
Below 20% RH for general materials, and below 15% RH for nylon, PA-CF and PET-CF, which is what QIDI prints on those data sheets. A sealed box with fresh desiccant and a cheap hygrometer inside is enough to hit both numbers. Ambient room air at 50% RH will slowly undo a full drying cycle in a matter of days for nylon.
Do I need to dry brand-new filament straight out of the bag?
Usually not for PLA, PETG, ABS or ASA if the vacuum bag was intact and the desiccant is still active. For nylon, PA-CF, PET-CF and PPS-CF it is worth doing anyway: those materials pick up moisture during the few minutes they spend on the bench, and a short cycle costs far less than a failed 20-hour print.
Can I dry filament in a microwave or with a hair dryer?
No. Neither method gives you controlled, even, sustained heat, and both create hot spots that deform the spool long before the core of the coil gives up its moisture. Use a filament dryer, a blast oven, a food dehydrator within its temperature range, or an in-print drying box.
Keep Your Filament Dry for Better 3D Prints
Good drying and storage practice matters as much as any slicer setting. Whether you use a commercial dryer, an oven, a food dehydrator or a homemade desiccant chamber, the goal is the same: get the water out at a temperature the material can survive, then keep it out. Regular checks and sealed storage prevent reabsorption. Do that consistently and you reduce printing defects, prolong the life of your filament, and spend less time diagnosing problems that were never really about the printer.
- Filament Drying Temperature and Time Chart
- What Is the Maximum Drying Temperature for PLA?
- The Importance of Dry Filament in 3D Printing
- Moisture: The Enemy of Print Quality
- Why Filaments Become Damp
- 4 Key Signs of Wet Filament
- Types of Filaments and Their Moisture Sensitivity
- Highly Moisture-Hungry Filaments: Nylon and TPU
- Middle-Ground Materials: PETG and PLA
- Moisture-Resistant Filaments: ABS
- Method 1: Using Commercial Filament Dryers
- Commercial Filament Dryer Mechanics
- Choosing Settings
- Method 2: Drying Filament in an Oven
- Oven Selection
- Drying Process
- Method 3: Drying Filament with a Food Dehydrator
- Adapting Your Dehydrator
- Setting Temperature and Time
- Pros and Cons
- Method 4: DIY Filament Drying Solutions
- Creating a Desiccant Chamber
- Using Silica Gel Packets
- Building a Heat Box
- Method 5: Drying Filament While You Print
- Does the QIDI Box Dry Filament While Printing?
- What About Filament Drying on the QIDI Q2?
- Filament Drying Guidelines for Specific 3D Printing Materials
- PLA and PLA-CF: Low-Temperature, Short-Duration Drying
- PETG: Medium-Heat, Moderate-Time Drying
- Nylon and Carbon-Fibre Nylon: High-Heat, Blast-Oven Drying
- Flexible Filaments: Gentle, Prolonged Drying
- Three Ways to Determine When Filament is Dry
- 1. Examine the Filament's Surface
- 2. Measure Weight Loss
- 3. Conduct a Test Print
- Strategies to Prevent Moisture Absorption During Printing
- 1. Use Filament Dry Boxes for Active Spools
- 2. Control Printing Environment Humidity
- 3. Perform Regular Maintenance Checks
- FAQs About Drying 3D Printer Filament
- How long does it take to dry filament?
- Can you over-dry filament?
- What humidity should filament be stored at?
- Do I need to dry brand-new filament straight out of the bag?
- Can I dry filament in a microwave or with a hair dryer?
- Keep Your Filament Dry for Better 3D Prints
Recommended products