 Q2
 QIDI Box
 Plus 4
 Q1 Pro
 X-Max 3


How to Print Ultra PA-CF25 Filament Perfectly?

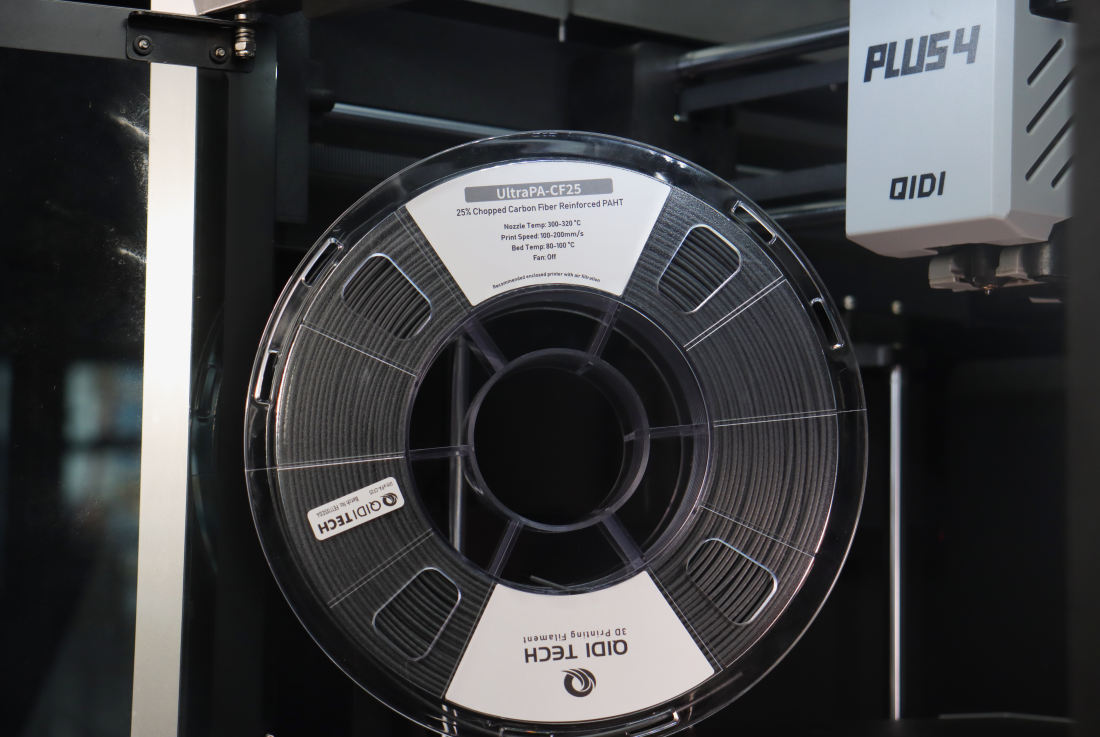
To print QIDI UltraPA-CF25 successfully, dry the spool at 80-100 °C for 4-6 hours, run the nozzle at 300-340 °C with the bed at 70-80 °C and speed between 30 and 200 mm/s, and use a hardened steel or bimetal nozzle of 0.4 mm or larger. Store it below 15% RH with desiccant, and anneal finished parts at 120 °C for more than six hours.
In 3D printing, filament properties directly determine the strength and accuracy of the print. QIDI UltraPA-CF25 is a professional filament designed for high-performance applications. Its 25% carbon fibre reinforced composite structure delivers high mechanical strength, high temperature resistance and dimensional stability. This guide covers its pre-printing drying, recommended print settings, hardware requirements, annealing and troubleshooting.
UltraPA-CF25 Specifications at a Glance
All values below are from QIDI's published data sheet for this filament. Print with them, not with generic nylon presets — a PA-CF composite behaves very differently from unfilled nylon in both temperature window and shrinkage.
| Parameter | Value |
|---|---|
| Material | Polyamide with 25% carbon fibre, PPA-coated filament surface |
| Drying before printing | 80-100 °C for 4-6 h (blast drying oven) |
| Nozzle temperature | 300-340 °C |
| Bed temperature | 70-80 °C |
| Print speed | 30-200 mm/s |
| Recommended nozzle | Hardened steel or bimetal, 0.4 / 0.6 / 0.8 mm |
| Not compatible | 0.2 mm nozzles |
| Density | 1.23 g/cm³ |
| Melting temperature | 237 °C |
| Heat deflection temperature | 196.9 °C |
| Tensile strength (X-Y) | 118.19 ± 3.82 MPa |
| Bending modulus (X-Y) | 9214.34 ± 249.80 MPa |
| Water absorption | 1.09% |
| Storage | < 15% RH, sealed with desiccant |
What UltraPA-CF25 Is, in One Paragraph
UltraPA-CF25 is a carbon-fibre-reinforced polyamide filament in which chopped carbon fibre makes up 25% of the compound and the strand surface carries a PPA coating. The carbon fibre supplies stiffness and dimensional stability; the PPA surface layer is what QIDI credits for the material's interlayer adhesion. The practical consequence of that composition is visible in one number: unfilled QIDI UltraPA has a heat deflection temperature of 72.5 °C, while UltraPA-CF25 reaches 196.9 °C. The fibre is doing the structural work at temperature, not the base polymer.
1. How to Dry UltraPA-CF25
Nylon-based filaments absorb water quickly once the bag is open, and UltraPA-CF25 has a saturation water absorption of 1.09%. Drying before printing is not optional for this material — a damp spool produces bubbling, stringing and a measurable loss of layer strength.
Drying procedure:
- Make sure the surface of the spool is clean and free of foreign matter.
- Place the spool in a blast drying oven.
- Set the oven to 80-100 °C for 4-6 hours. The exact time depends on how damp the filament is.
- Start drying, then move the spool straight into a sealed container or a heated feed system once the cycle ends.
Two cautions matter here. First, do not dry the spool at annealing temperatures. The 120 °C figure used later in this guide applies to finished printed parts on a tray, not to a plastic spool that will soften and distort. Stay inside 80-100 °C for the spool. Second, store the filament in a sealed container with desiccant and keep relative humidity in the container below 15% RH. For the full drying chart across every material, see the filament drying guide.

2. Recommended Printing Parameters and Accessories
The machine used is QIDI Plus4 as an example.
Recommended accessories:
- Build plate: use a QIDI PEI plate or smooth PEI plate.
- Nozzle: use a tungsten carbide nozzle (0.4 / 0.6 / 0.8 mm) or a bimetal nozzle (0.4 / 0.6 / 0.8 mm).
Recommended printing parameters:
- Nozzle temperature: 300-340 °C
- Bed temperature: 70-80 °C
- Printing speed: 30-200 mm/s
Why a Brass Nozzle Will Not Survive This Material
Chopped carbon fibre is abrasive in the same way glass fibre and mineral-filled composites are: hard particles suspended in a soft matrix. The polymer passes through the bore harmlessly; the fibre ends scrape it wider on the way out. A brass nozzle running PA-CF loses its bore geometry within a small number of spools, and the failure mode is gradual — over-extrusion and lost detail long before anything blocks. Hardened steel and bimetal nozzles solve it outright. QIDI also lists 0.2 mm nozzles as incompatible with this filament, because a 0.2 mm bore cannot reliably pass fibre bundles of this length.
Which QIDI Printers Suit UltraPA-CF25
Three hardware conditions have to be met: a hotend that reaches 340 °C, an abrasion-resistant nozzle, and — for anything larger than a small bracket — a heated chamber to control warping while the part cools. Every current QIDI machine has a 370 °C hotend and ships with a bimetal nozzle, so the differentiator is the chamber.
| Printer | Hotend max | Chamber | Suitability for UltraPA-CF25 |
|---|---|---|---|
| Q2C | 370 °C | Flame-retardant enclosure, no chamber heater | Small parts only; expect more warping on large flat footprints |
| Q2 | 370 °C | 65 °C, 2nd gen independent heating | Suitable, 270 × 270 × 256 mm build volume |
| Plus 5 | 370 °C | 65 °C, 3rd gen independent heating | Suitable, 320 × 320 × 300 mm build volume |
| Max4 | 370 °C | 65 °C active | Suitable, 390 × 390 × 340 mm for large functional parts |
The chamber matters because polyamide shrinks as it cools and a temperature gradient through a tall part converts that shrinkage into internal stress. Holding the chamber at 65 °C keeps the whole part near the same temperature while it builds, which is why chamber heating prevents cracking in nylon parts. On the Q2C, which has a sealed but unheated enclosure, keep footprints small and expect to work harder on bed adhesion.
3. How to Anneal UltraPA-CF25 Prints
Annealing is the practice of heating and then cooling a material to change its physical properties. In 3D printing, annealing relieves the thermal stress frozen into a part as it cooled, improving strength and heat resistance. The effect depends on filament type, annealing temperature and duration, and for complex geometry improper handling can cause the part to deform or warp.
For best results, use a blast drying oven.
- Place the parts on a tray so they heat evenly, supported flat rather than resting on thin edges.
- Heat the oven to 120 °C.
- Put the tray in the oven and hold the parts there for more than 6 hours.
- Turn the oven off and let the parts cool down inside it. A slow cool is part of the process; pulling hot parts into room air reintroduces the stress you just removed.
- Take out the tray and the parts once they are at room temperature.
Annealing is worth doing when a part will see sustained load or elevated temperature in service. It is not worth doing on a cosmetic part or a loose-tolerance fixture, because dimensions can shift slightly as internal stress releases. If a part must hold a tight fit, anneal a test piece first and measure the change before committing the batch.

4. Troubleshooting UltraPA-CF25
Almost every problem with this material traces back to one of three things: moisture, insufficient heat, or a cooling gradient. The table below maps the symptom to the cause worth checking first.
| Symptom | Most likely cause | Correction |
|---|---|---|
| Popping or hissing at the nozzle, fuzzy surface | Moisture in the filament | Dry at 80-100 °C for 4-6 h, then print from sealed or heated storage |
| Layers split apart under light load | Nozzle at the low end of the range, or chamber cold | Raise nozzle toward 330-340 °C; enable chamber heating |
| Corners lift off the plate | Uneven cooling, weak first-layer adhesion | Chamber to 65 °C, bed 80 °C, add a brim, use adhesive on the PEI plate |
| Cracks appearing hours after the print finished | Residual stress from a steep cooling gradient | Keep the door closed until the chamber is near ambient; anneal the part |
| Gradual over-extrusion, loss of fine detail | Nozzle bore worn by carbon fibre | Replace with hardened steel or bimetal; do not run brass on PA-CF |
| Intermittent under-extrusion or blockage | Nozzle too small, or degraded material in the melt zone | Use 0.4 mm or larger, never 0.2 mm; purge fully when switching materials |
| Parts weaker than the data sheet suggests | Test direction, not material fault | Published 118 MPa is X-Y; Z-axis strength is always lower, so orient load paths in plane |
5. What Are the Advantages of UltraPA-CF25?
QIDI UltraPA-CF25 is a professional grade 3D printing filament designed for industrial applications that require high performance and precision.
a. Strong mechanical performance for demanding parts
- The core is reinforced with 25% carbon fibre, raising the tensile strength and rigidity of printed parts to 118.19 ± 3.82 MPa and a bending modulus of 9214.34 ± 249.80 MPa in the X-Y plane, so parts stay strong and resist deformation in high-stress environments.
- Good impact resistance means printed parts remain stable and intact when subjected to external forces and collisions.
b. Industrial grade precision, reducing print failure rate
- The carbon fibre reinforcement reduces warping and deformation during printing, giving higher dimensional accuracy and easier assembly. This is what makes it usable for production fixtures and engineering applications rather than prototypes only.
c. Interlayer adhesion supported by the PPA surface layer
- A reinforced fibre coating technology wraps a layer of PPA base material around the surface of the filament, which QIDI credits for the material's improved interlayer adhesion.
- Even thin-walled structural components retain high mechanical stability.
d. High temperature resistance, expanding the application range
- A heat deflection temperature of 196.9 °C suits functional components in hot environments such as automotive parts and industrial equipment. For comparison, unfilled UltraPA nylon reaches 72.5 °C, and PETG is far lower still.
It also offers good chemical corrosion resistance and wear resistance, maintaining stable mechanical properties over long service in demanding environments.

FAQs About UltraPA-CF25
What temperature should UltraPA-CF25 be dried at?
80-100 °C for 4-6 hours in a blast drying oven, which is QIDI's published specification. Do not use 120 °C for the spool: that temperature belongs to the annealing procedure for finished parts and will soften a plastic spool. After drying, store the filament sealed with desiccant below 15% RH.
Is UltraPA-CF25 a PPA filament?
Its base polymer is a carbon-fibre-filled polyamide, and the filament surface carries a PPA coating applied by a reinforced fibre coating process. So it is a PA-CF with a PPA surface layer rather than a bulk PPA compound. If you are looking specifically for a bulk high-temperature composite, the PPS-CF guide covers the higher-temperature option in the range.
What is the difference between UltraPA and UltraPA-CF25?
Carbon fibre content. UltraPA is unfilled nylon: nozzle 260-280 °C, heat deflection temperature 72.5 °C, water absorption 2.10%. UltraPA-CF25 adds 25% carbon fibre: nozzle 300-340 °C, heat deflection temperature 196.9 °C, water absorption 1.09%. The CF version is stiffer, far more heat resistant and less prone to warping, but it needs a hotter nozzle and an abrasion-resistant one.
Do I need a heated chamber to print PA-CF?
For small parts, no. For anything with a large flat footprint or a tall thin wall, effectively yes — polyamide shrinks as it cools, and an uneven cooling gradient converts that shrinkage into warping or delayed cracking. A 65 °C actively heated chamber keeps the whole part near one temperature during the build. Background on the mechanism is in the nylon 3D printing guide.
Why are my parts weaker than the published tensile strength?
Test direction. The 118.19 MPa figure is measured in the X-Y plane, where the carbon fibres lie along the extrusion paths. Strength across the layers in Z is governed by interlayer bonding rather than by the fibres, and is always lower in any FFF part. Orient the part so that the main load runs in plane, and increase wall count rather than infill for load-bearing features. The wider material trade-offs are covered in the guide to choosing industrial composites.
Summary
QIDI UltraPA-CF25 is an industrial grade 3D printing filament that combines high strength, high temperature resistance and dimensional stability. Dry it at 80-100 °C, print it at 300-340 °C on a hardened steel or bimetal nozzle of 0.4 mm or larger, keep the chamber warm for anything sizeable, store it below 15% RH, and anneal parts destined for load or heat. Get those five things right and the material delivers the performance its data sheet promises. The rest of the engineering range sits in industrial grade composites.
- UltraPA-CF25 Specifications at a Glance
- What UltraPA-CF25 Is, in One Paragraph
- 1. How to Dry UltraPA-CF25
- 2. Recommended Printing Parameters and Accessories
- Why a Brass Nozzle Will Not Survive This Material
- Which QIDI Printers Suit UltraPA-CF25
- 3. How to Anneal UltraPA-CF25 Prints
- 4. Troubleshooting UltraPA-CF25
- 5. What Are the Advantages of UltraPA-CF25?
- FAQs About UltraPA-CF25
- What temperature should UltraPA-CF25 be dried at?
- Is UltraPA-CF25 a PPA filament?
- What is the difference between UltraPA and UltraPA-CF25?
- Do I need a heated chamber to print PA-CF?
- Why are my parts weaker than the published tensile strength?
- Summary
Recommended products