 Q2
 QIDI Box
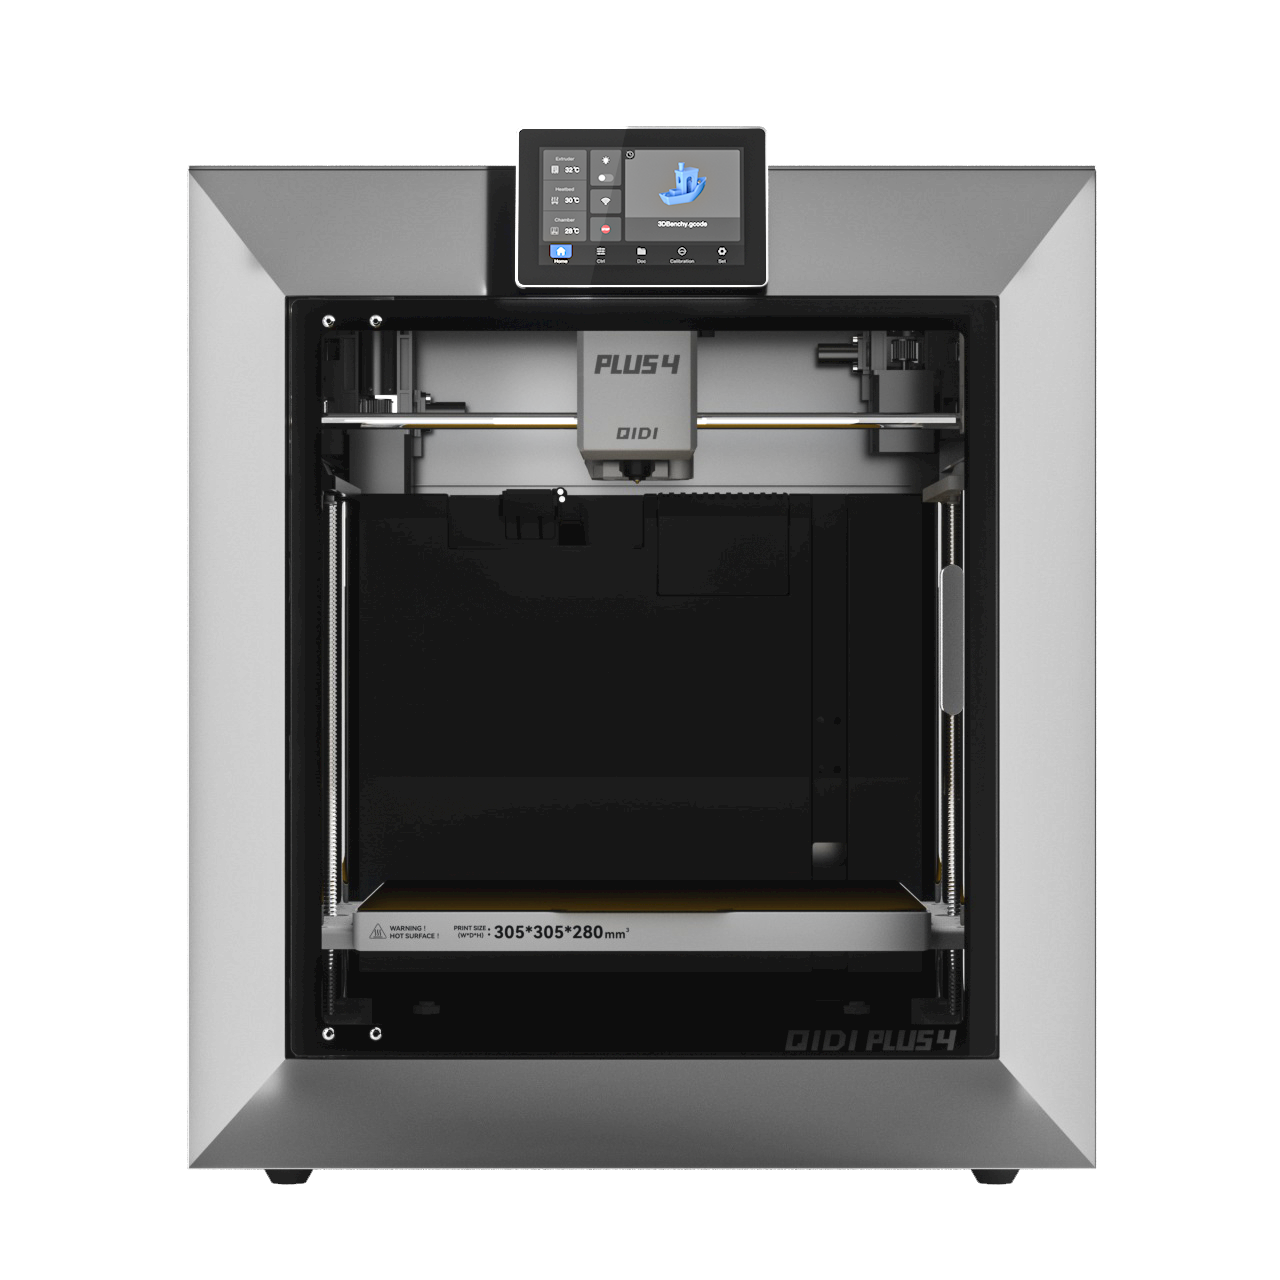 Plus 4
 Q1 Pro
 X-Max 3


Why Makers Choose QIDI 3D Printers for Rapid Prototyping


A prototype can look clean and still fail during assembly. Poor fit, warped walls, weak tabs, and slow reprints can turn one design change into a lost weekend. Makers need a 3D printer for rapid prototyping that keeps each revision moving while providing enough accuracy, material capability, and consistency to answer a specific design question before they commit more time or money.

What Makers Really Need From a 3D Printer for Rapid Prototyping
Useful prototypes answer focused questions. One print may check enclosure clearance, while another tests a latch through repeated cycles. Defining that question first helps a maker choose the right material, orientation, settings, and test method for the job.
Choosing a 3D printer for rapid prototyping comes down to five capabilities:
- Reliable first layers: Automatic leveling and consistent nozzle offset reduce setup work and material loss between revisions.
- Suitable material options: PLA suits concept and fit models. PETG adds toughness. ABS, ASA, PA, PC, and reinforced filaments address tougher thermal or mechanical demands when the complete setup supports them.
- Enough usable build volume: A one-piece prototype can preserve alignment. A larger bed can also hold several versions of a small component.
- Accessible process controls: Layer height, walls, infill, orientation, support, cooling, and temperature all affect what a prototype can prove.
- Repeatable output: Motion stability, thermal control, dry filament, and documented settings help comparable parts produce useful test data.
Maximum toolhead speed provides only part of the time picture. Small features, detailed surfaces, engineering filaments, and material flow limits can reduce practical speed. Makers gain a clearer view by tracking the full cycle, including preparation, printing, inspection, failed jobs, and post-processing.
How 3D Printing Speeds Up the Journey From Concept to Functional Prototype
Desktop FDM printing keeps design and physical testing in the same workspace. A shorter feedback loop is most useful while dimensions, mechanisms, and assembly details are still changing.
Move CAD Changes Into Physical Testing
A CAD revision can become a test part without waiting for tooling, machining access, or outside production. A 3D printer for rapid prototyping can expose interference, blocked fasteners, poor cable routes, uncomfortable grips, and excessive tab deflection. Each observation gives the next CAD revision a specific purpose.
Print Only the Feature Under Review
A complete assembly is often unnecessary during early testing. A small section can isolate a hinge, snap fit, screw boss, bearing seat, gasket channel, or cable opening. Once that feature works, the next print can examine its interaction with the larger assembly. Full-size builds are then reserved for revisions that have passed smaller checks.
Keep Each Revision Comparable
Keep the material, orientation, layer height, and slicer profile consistent while adjusting one hole diameter, rib thickness, or clearance value. Measure the same feature and apply the same load after every print. A controlled revision makes the cause of an improvement easier to identify.

Why QIDI 3D Printers Work Well for Functional Prototyping
For makers choosing a 3D printer for rapid prototyping, our current lineup combines enclosed CoreXY structures, direct extrusion, automatic leveling, and high nozzle-temperature ceilings.
Control the Temperature Around the Part
ABS, ASA, PA, and PC can lift or develop layer separation on larger parts as they cool. The Q2, Plus5, and Max4 provide active chamber heating up to 65°C. The Q2C has a passive enclosure that blocks drafts but does not include an active chamber heater. Chamber heat helps control thermal variation, though orientation and the material profile still matter.
Match the Extrusion Setup to the Filament
The Q2C, Q2, Plus5, and Max4 have nozzle-temperature ceilings up to 370°C and use direct extrusion. The full setup still determines material compatibility. The nozzle, build surface, drying routine, ventilation plan, and slicer profile must suit the filament and its specified processing range.
Inspect the Toolpath Before Printing
QIDI Studio combines slicing and printer control. Its preview can expose unsupported regions, missing thin walls, excessive support, or layer lines placed across a loaded feature. Camera and detection capabilities vary by model, so users should confirm the monitoring functions included with their printer.
Keep Moisture Management Separate From Chamber Control
The optional QIDI Box supports drying during printing, automatic refill, and multi-material workflows on compatible machines. It can support snap-away or dissolvable supports when the material pair, machine, and profile are compatible. Chamber heating stabilizes the air around the part. Filament drying manages spool moisture that can cause bubbles, stringing, rough surfaces, or inconsistent extrusion.
Which QIDI 3D Printer Fits Different Maker Projects?
Choosing the right QIDI 3D printer for rapid prototyping depends on part size, material behavior, workspace, and the purpose of the test. Maximum specifications alone do not show which machine fits a recurring workload.
|
Model |
Key Hardware |
Strong Project Fit |
Main Selection Boundary |
|
270 × 270 × 256 mm build volume, enclosed structure, 370°C nozzle ceiling, no active chamber heater |
Concept models, ergonomic samples, PLA or PETG fit checks, hobby mechanisms, early functional parts |
The passive enclosure offers less thermal control for large parts made from high-shrink engineering filaments |
|
|
270 × 270 × 256 mm build volume, 370°C nozzle ceiling, active chamber heating up to 65°C |
Compact brackets, housings, jigs, fixtures, and temperature-sensitive materials |
The build envelope may constrain long fixtures and large one-piece housings |
|
|
320 × 320 × 300 mm build volume, 370°C nozzle ceiling, active chamber heating up to 65°C |
Medium and large functional prototypes, several test pieces, sizable enclosures, and engineering-material development |
Large jobs carry higher time and material costs, so local feature tests remain useful |
|
|
390 × 390 × 340 mm build volume, 370°C nozzle ceiling, active chamber heating up to 65°C, toolhead speed rated up to 800 mm/s |
Large assemblies, long fixtures, full-scale shells, and multi-part batches |
It needs more machine space, and practical speed varies with geometry and filament |
Q2C and Q2 share the same build volume, so thermal control is the main dividing point between them. Plus5 gives larger housings and small batches additional room within a desktop format. Max4 becomes valuable when a one-piece build can preserve alignment, sealing surfaces, or assembly accuracy across a substantially larger part.
A Typical Maker Workflow With a QIDI 3D Printer
Using a 3D printer for rapid prototyping becomes more effective when the CAD revision, print settings, and test result stay connected.
-
Define the validation goal. Write one sentence describing the decision the print must support. Examples include, “Does the connector clear the enclosure wall?” or “Can the latch complete 100 manual cycles?”
-
Prepare the CAD model for FDM. Check wall thickness, overhangs, hole orientation, assembly access, and load direction. Add fillets around stressed corners and isolate uncertain features as smaller test pieces when useful.
-
Choose a material that matches the test. PLA is efficient for geometry and presentation. PETG suits many tough, general-purpose parts. ABS and ASA can serve warmer or outdoor conditions. PA, PC, and reinforced polymers may fit demanding mechanical tests when the printer, nozzle, drying process, and environment support the chosen filament.
-
Slice around the validation goal. Select the printer and filament profile in QIDI Studio, then set layer height, walls, infill, support, and orientation. Cosmetic models may favor finer layers. Loaded parts may need additional walls and an orientation that places critical forces along stronger paths.
-
Review the toolpath. Check the layer preview for unsupported regions, thin features, internal gaps, seam placement, and unexpected support. Confirm material use and job time before sending the file.
-
Print and inspect. Watch the first layer, follow the machine and filament instructions, and examine the finished part for warping, cracks, inconsistent extrusion, and dimensional error. Record visible defects before post-processing changes their appearance.
- Run the planned test. Keep the fixture, load, cycle count, and measurement method consistent across revisions. Label each part with its CAD revision, material, orientation, and profile version.
- Change one major variable. Update the geometry or one relevant process setting, then repeat the same test. This keeps the effect of the revision easier to identify.
A failed part can still point to a specific improvement. A broken tab may expose a poor load path, while a warped corner may indicate a thermal or orientation issue. Recording the failure mode makes the next CAD or process change easier to choose.

What a 3D-Printed Prototype Can and Cannot Validate
A 3D printer for rapid prototyping produces evidence for a defined design decision. One print cannot prove that the final product is safe, durable, or ready for production.
|
A Functional FDM Prototype Can Evaluate |
Additional Validation May Be Required For |
|
Assembly order and tool access |
Production-process surface finish and tolerances |
|
Basic motion, reach, grip, and user interaction |
Long-term creep, fatigue, and temperature aging |
|
Interference, clearance, and fastener placement |
Chemical resistance, weathering, and reliable sealing |
|
Direction-specific loads under a documented test |
Isotropic strength or behavior of a molded, cast, or machined material |
|
Repeatability across several prints made under the same conditions |
Safety-critical performance and regulatory compliance |
Layer bonding makes FDM strength direction-dependent, and printed filament may behave differently from the intended production material. Record the material, orientation, settings, test method, and failure mode for every important revision. Critical parts still require an engineering review and a validation plan suited to their final use.
FAQs About QIDI 3D Printers for Makers
Q1. What Wall Count Should I Use for a Functional FDM Prototype?
A practical baseline is three or four walls with a 0.4 mm nozzle, adjusted for the expected load and geometry. Dense infill can add print time with limited benefit. Thin ribs, fastener bosses, and impact zones may need fillets, local reinforcement, or a different orientation.
Q2. How Much Clearance Should I Leave Between Mating Printed Parts?
Many tuned FDM assemblies use about 0.2 to 0.4 mm of clearance per side for a movable fit. The correct value still depends on material, orientation, feature size, and printer calibration. Print a small tolerance coupon with several gaps and apply the measured result to the CAD model.
Q3. Can I Install Threaded Metal Inserts in a QIDI-Printed Prototype?
Yes. Heat-set inserts work well in thermoplastic prototypes that need repeated assembly. Design the boss around the insert manufacturer's recommended hole geometry, leave enough material around the hole, and practice on a spare coupon to confirm the insertion temperature, alignment, and final depth before working on the complete part.
Q4. Should I Use a 0.4 mm or 0.6 mm Nozzle for Prototyping?
A 0.4 mm nozzle offers a useful balance of detail, speed, and profile availability for most prototypes. A compatible 0.6 mm nozzle can shorten large prints and handle thicker walls or abrasive composites more comfortably. Select the correct nozzle profile and confirm dimensional performance after the change.
Q5. How Should I Check Accuracy Before Printing a Large Prototype?
Print a small coupon containing the project's critical holes, slots, walls, or mating features in the same material and orientation planned for the full part. Let it cool, measure it with suitable tools, and adjust the CAD dimensions or slicer compensation only after identifying a consistent deviation.
- What Makers Really Need From a 3D Printer for Rapid Prototyping
- How 3D Printing Speeds Up the Journey From Concept to Functional Prototype
- Move CAD Changes Into Physical Testing
- Print Only the Feature Under Review
- Keep Each Revision Comparable
- Why QIDI 3D Printers Work Well for Functional Prototyping
- Control the Temperature Around the Part
- Match the Extrusion Setup to the Filament
- Inspect the Toolpath Before Printing
- Keep Moisture Management Separate From Chamber Control
- Which QIDI 3D Printer Fits Different Maker Projects?
- A Typical Maker Workflow With a QIDI 3D Printer
- What a 3D-Printed Prototype Can and Cannot Validate
- FAQs About QIDI 3D Printers for Makers
- Q1. What Wall Count Should I Use for a Functional FDM Prototype?
- Q2. How Much Clearance Should I Leave Between Mating Printed Parts?
- Q3. Can I Install Threaded Metal Inserts in a QIDI-Printed Prototype?
- Q4. Should I Use a 0.4 mm or 0.6 mm Nozzle for Prototyping?
- Q5. How Should I Check Accuracy Before Printing a Large Prototype?
Recommended products