 Q2



Why Geeks Love QIDI 3D Printers: Klipper, Open-Source Software, and Room to Tinker


Factory presets can produce clean prints, yet experienced makers soon want deeper control. They need access to motion tuning, material profiles, macros, slicer settings, and the configuration behind each result. QIDI 3D printers combine Klipper-based control, capable hardware, and open-source software with a supported factory workflow, giving technically curious users room to experiment without rebuilding a machine from the ground up.
What Advanced Users Want Beyond Plug-and-Print Convenience
Advanced users still value reliable first layers and proven factory profiles. They also need enough access to investigate defects, tune specific materials, automate repeated actions, and restore a working configuration after testing.

A Stable Baseline for Controlled Tests
A dependable factory profile provides a reference for every later adjustment. When a print develops poor corners, ringing, weak layer bonding, or inconsistent extrusion, you can compare the new settings with a known-good result. Changing Pressure Advance, cooling, acceleration, or flow one variable at a time also makes the effect of each adjustment easier to identify.
Documentation That Supports Diagnosis
Configuration access has limited value when users cannot find model-specific instructions. We maintain Wiki pages, firmware packages, software downloads, and public code repositories for supported machines. These resources help you determine if a problem comes from the slicer, material, motion system, or hardware before editing configuration files or replacing parts.
How QIDI Hardware Supports Material and Process Experiments
Software settings can only work within the printer's mechanical and thermal limits. Motion design affects movement behavior, while chamber control, nozzle size, and filament handling shape the materials and part types each model can process reliably.
CoreXY Motion and Build Environment
Across our current lineup, QIDI 3D printers use CoreXY motion systems. The Q2, Plus4, Plus5, and Max4 provide enclosed build environments for greater temperature stability. The open-frame Q2C focuses on common materials and accessible process tuning without an actively heated chamber.
Active Chamber Heating for Engineering Materials
The enclosed heated-chamber models support active chamber temperatures up to 65°C and hotend temperatures up to 370°C. Controlled chamber heat can reduce uneven cooling in ABS, ASA, PA, PC, and other engineering materials. Consistent results still depend on dry filament, suitable bed preparation, part geometry, and a material-specific profile.
Nozzle Sizes for Detail and Throughput
Current machines ship with a 0.4 mm nozzle, while compatible profiles support 0.2, 0.6, and 0.8 mm options on selected models. A 0.2 mm nozzle suits fine features and small text. Larger nozzles support wider lines and higher material flow on large parts. Each change requires matching line width, layer height, temperature, flow, and Pressure Advance settings.
QIDI Box for Multi-Material Workflows
The QIDI Box holds four spools, dries supported filament at up to 65°C, and can switch to a backup spool when material runs out. Up to four units can handle 16 colors or materials with the required expansion hardware. Feed reliability still depends on spool dimensions and filament properties. Generic flexible TPU, cardboard spools without an adapter, and some specialty filaments may need direct feeding.
Why Klipper Appeals to Advanced 3D Printing Users
Klipper gives experienced makers access to the settings that control motion, extrusion, and repeated printer actions. On QIDI 3D printers, we customize this open-source foundation for each machine's controller, screen, sensors, heaters, and factory workflow.
Input Shaping for Mechanical Resonance
Input Shaping compensates for measured mechanical resonance and can reduce ringing or ghosting on printed walls. Its useful values depend on the printer's physical behavior. Changes to belts, toolhead mass, motion components, or machine placement may justify a new resonance test.
Pressure Advance for Extrusion Control
Pressure Advance adjusts extrusion during acceleration and deceleration. Correct calibration can produce cleaner corners and reduce excess material around direction changes. Filament type, color, nozzle size, temperature, and extrusion hardware can all affect the appropriate value, so a setting from another profile may produce different results.
Configuration Files and G-Code Macros
Readable configuration files make machine behavior easier to inspect and document. Fluidd provides browser access to printer status, files, temperatures, console commands, and supported configuration areas. G-code macros can combine repeated commands into a consistent sequence, while configuration backups make it easier to compare changes or return to a working setup.

QIDI Studio, Orca Slicer, and Other Software Options
Choose a slicer according to the device controls and calibration tools you need. Always match the printer profile to the machine, nozzle, and firmware version.
QIDI Studio for Integrated Device Control
QIDI Studio is our primary application for current machines. It combines model-specific profiles, calibration tools, printer connection, multi-device functions, and QIDI Box management. Its source code is publicly available under the AGPL v3 license through our open-source repositories.
QIDI Slicer and Orca Slicer for Flexible Workflows
QIDI Slicer remains useful for compatible high-speed and earlier models whose owners prefer its parameter layout. Orca Slicer includes profiles for many QIDI machines and offers community-developed calibration tools. Both QIDI Studio and Orca Slicer support 3MF projects, allowing models and many project settings to move between them. Machine-specific commands should still be reviewed before printing.
QIDI Box Management and Profile Checks
QIDI Studio can read QIDI Box slots, map project materials, calculate flushing volumes, and control supported drying settings. Orca Slicer can prepare multi-color geometry for a compatible printer, while direct QIDI Box control remains within QIDI Studio.
Before sending a long print, confirm the machine model, nozzle diameter, build volume, start and end G-code, chamber controls, and material temperatures. A profile may recognize the printer while still lacking a recently added macro or hardware function.
What Advanced Users Can Tune on a QIDI 3D Printer
Each experiment should connect a visible problem to a limited group of settings. Cleaner corners, stronger layer bonding, shorter production time, and a steadier first layer require different tests. Focus on one of the following areas during each test.
- Material profiles: Tune nozzle, bed, and chamber temperatures along with flow ratio, cooling, and maximum volumetric speed for a specific filament. Dry hygroscopic materials before calibration because wet filament can distort every later result.
- Pressure Advance: Recalibrate after meaningful changes to filament, nozzle, temperature, or extrusion hardware. Values copied from a different material or color may produce inconsistent corners because viscosity and elasticity vary.
- Input Shaping: Review resonance settings after changes that affect moving mass, belts, or toolhead components. A calibration measurement provides a starting value, while printed surfaces show how well that value works at the intended speed.
- Speed and acceleration: Increase them in measured steps while checking flow capacity, cooling, layer bonding, motor behavior, and surface artifacts. Maximum toolhead speed describes motion capability. Real print speed remains limited by geometry, extrusion flow, and material behavior.
- Nozzle size: Choose a 0.2 mm nozzle for small features or a larger supported nozzle for wider lines and faster large parts. Match the slicer profile, then review flow, temperature, Pressure Advance, and first-layer behavior.
- Macros and adaptive meshing: Supported Wiki procedures show how configuration files, Fluidd, and features such as KAMP can be used on specific models. Our Q2 KAMP instructions provide one example of model-specific configuration access.
Record the printer model, firmware version, slicer version, nozzle, filament condition, changed value, and visible outcome for every useful test. A short test log turns a successful print into a repeatable profile and makes failed tests easier to diagnose.
How Much Tinkering Freedom Do QIDI Printers Actually Offer?
Our QIDI 3D printers use customized versions of Klipper and Moonraker alongside model-specific services. Users can work with profiles, macros, Fluidd, configuration files, and supported firmware packages. The factory control stack remains tied to each machine's hardware.
We advise against updating Klipper or Moonraker through KIAUH or Git. Public upstream releases may conflict with the mainboard, screen, or customized services, and problems caused by unsupported firmware changes may fall outside warranty and remote assistance. The QIDI software and firmware notice explains this limitation directly.
Safe tuning begins with a backup and a reversible plan. Save the original configuration, record each edit, and change one variable per test. Use the firmware package and Wiki instructions written for the exact model when recovery is needed. Physical upgrades require equal care because nozzle length, connectors, sensors, heater power, and mounting geometry vary between printers.
Users seeking unrestricted replacement of the complete firmware stack or a fully open mechanical design should account for the model-specific boundaries before purchasing.
Which QIDI 3D Printer Fits Different Advanced Users?
Choose among current QIDI 3D printers according to build volume, chamber requirements, workspace, and the materials you plan to test.
|
Model |
Best Fit |
Useful Advanced Features |
Important Boundary |
|
Budget-focused tuning with PLA, PETG, and common materials |
270 × 270 × 256 mm build area, 370°C hotend, automatic leveling, QIDI Box compatibility |
Open-frame design with no active chamber heater; camera and filtration are optional |
|
|
Compact engineering-material work |
270 × 270 × 256 mm build area, 65°C active chamber, 370°C hotend, AI camera, filtration, QIDI Box support |
Smaller build area than the Plus and Max lines |
|
|
Established mid-size, high-temperature workflows |
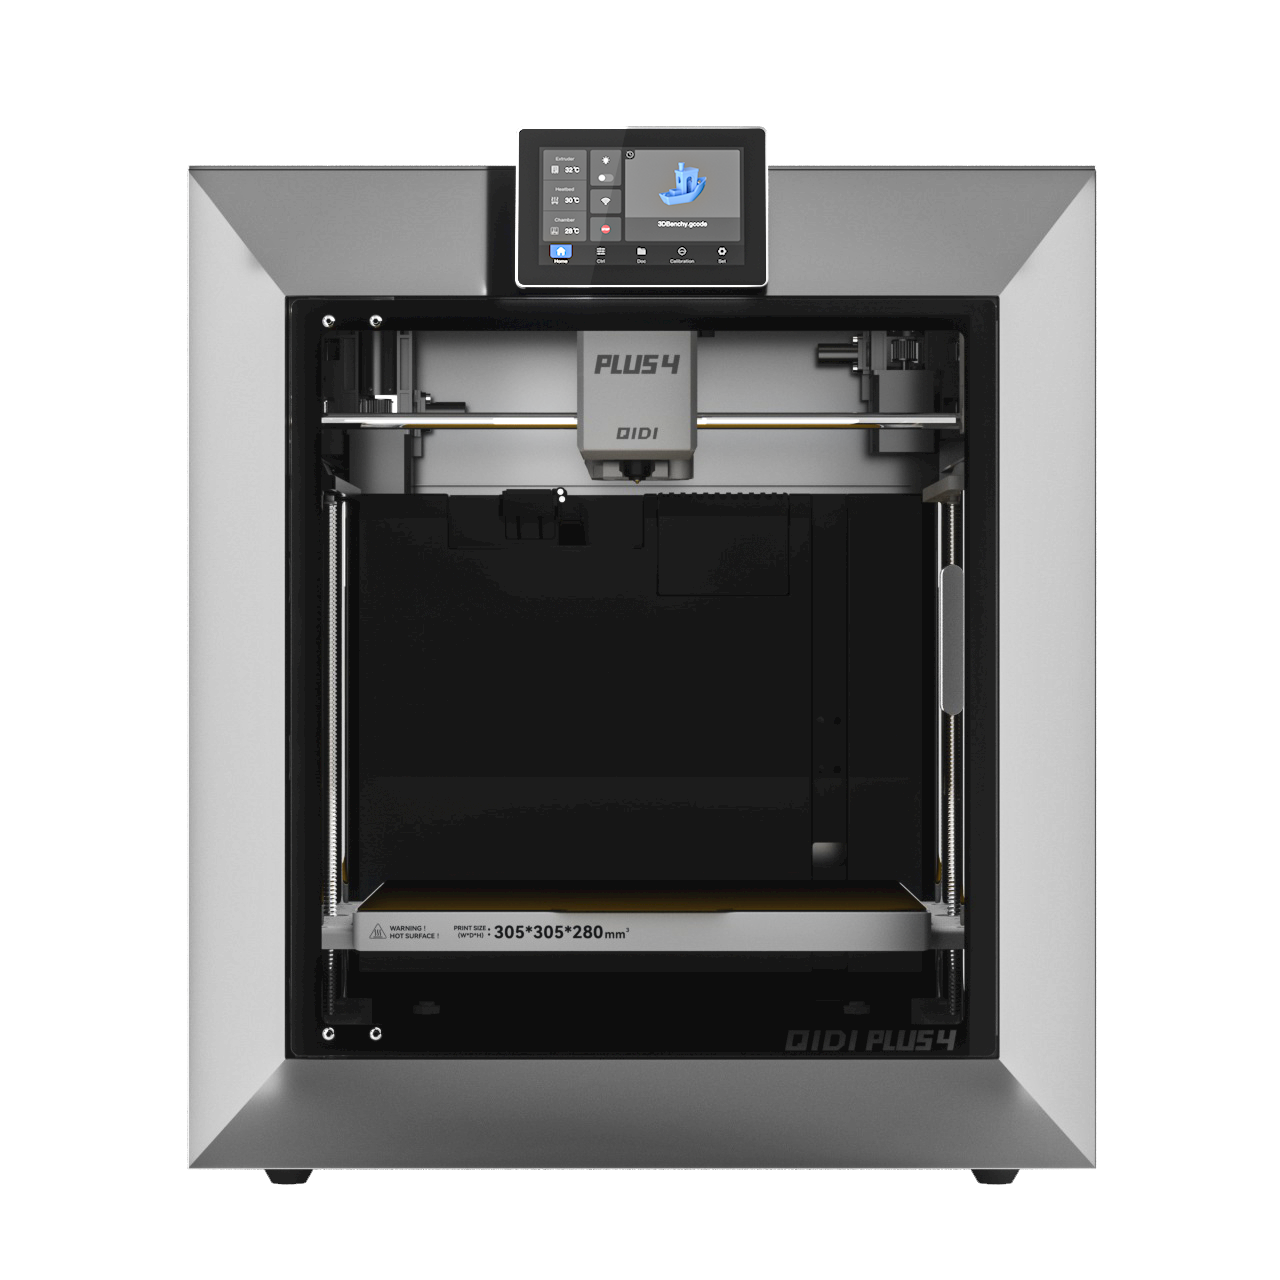
305 × 305 × 280 mm build area, 65°C active chamber, 370°C hotend, camera, filament monitoring, QIDI Box support |
Availability varies by region as Plus5 enters the range |
|
|
Broad advanced use with newer mid-size hardware |
320 × 320 × 300 mm build area, third-generation 65°C chamber, 370°C hotend, updated motion system, AI monitoring |
Requires more desk space and power than compact models |
|
|
Large prototypes and high-volume build plates |
390 × 390 × 340 mm build area, 65°C chamber, 370°C hotend, up to 800 mm/s toolhead speed, AI monitoring |
Large parts demand substantial workspace and careful thermal control |
Plus5 balances build capacity, chamber control, and current hardware. Q2 brings similar high-temperature capability to a smaller workspace. Max4 fits projects that exceed the Plus platform or place many parts on one build plate.
Q2C suits slicer, Klipper, and multi-color experiments with common materials. Frequent ABS, ASA, PA, PC, or composite printing favors an actively heated model. Plus4 remains useful for established workflows, subject to regional availability.
Who Is a QIDI 3D Printer Best Suited For?
QIDI 3D printers fit makers who want a dependable factory workflow and access to meaningful process controls. The strongest fit includes users who enjoy calibration, create functional prototypes, print engineering materials, manage several material profiles, or need large enclosed build volumes.
Educators and small workshops can also benefit from repeatable profiles, local device access, and model-specific documentation. A supported machine reduces setup work, while configuration access leaves room for lessons or process development involving motion, extrusion, thermal behavior, and slicing.
The fit is weaker for users whose main goal is replacing the full firmware stack, redesigning the motion system, or treating the printer as an unrestricted open-hardware project.
FAQs About QIDI Klipper and Open-Source Software
Q1. Do QIDI Klipper Printers Need a Separate Raspberry Pi?
No. Current Klipper-based QIDI models include the computing hardware needed to run the factory control environment. You can reach supported Fluidd and network functions through the printer's onboard system, which removes the need to purchase, install, and maintain a separate Raspberry Pi host.
Q2. Can a QIDI Printer Work Without a Cloud Connection?
Yes. Supported models can print from a USB drive and provide local connection options through Ethernet or Wi-Fi, depending on the machine. Cloud features add remote convenience. Normal slicing and printing do not require a continuous internet connection. Confirm the available ports on your selected model.
Q3. Can QIDI Printers Use Third-Party Filament?
Yes. QIDI printers use standard 1.75 mm filament and can run compatible materials from other suppliers. Create or adjust a suitable profile, check the printer's temperature and nozzle requirements, and dry moisture-sensitive filament. QIDI Box compatibility also depends on spool size and filament flexibility.
Q4. Does Changing Nozzle Size Require a Firmware Modification?
Usually, no. A supported nozzle-size change calls for the correct nozzle and a matching slicer profile. Update nozzle diameter, line width, layer height, flow, and related calibration values. Use a nozzle designed for the exact printer and hotend because dimensions and mounting details can differ.
Q5. Can QIDI Studio Import STEP Files From CAD Software?
Yes. QIDI Studio can import STEP files and preserve assembly relationships through Assembly View. This keeps component placement available during preparation and can avoid an early mesh conversion. Check scale, orientation, tolerances, and the placement of every component before slicing the final build plate.
- What Advanced Users Want Beyond Plug-and-Print Convenience
- A Stable Baseline for Controlled Tests
- Documentation That Supports Diagnosis
- How QIDI Hardware Supports Material and Process Experiments
- CoreXY Motion and Build Environment
- Active Chamber Heating for Engineering Materials
- Nozzle Sizes for Detail and Throughput
- QIDI Box for Multi-Material Workflows
- Why Klipper Appeals to Advanced 3D Printing Users
- Input Shaping for Mechanical Resonance
- Pressure Advance for Extrusion Control
- Configuration Files and G-Code Macros
- QIDI Studio, Orca Slicer, and Other Software Options
- QIDI Studio for Integrated Device Control
- QIDI Slicer and Orca Slicer for Flexible Workflows
- QIDI Box Management and Profile Checks
- What Advanced Users Can Tune on a QIDI 3D Printer
- How Much Tinkering Freedom Do QIDI Printers Actually Offer?
- Which QIDI 3D Printer Fits Different Advanced Users?
- Who Is a QIDI 3D Printer Best Suited For?
- FAQs About QIDI Klipper and Open-Source Software
- Q1. Do QIDI Klipper Printers Need a Separate Raspberry Pi?
- Q2. Can a QIDI Printer Work Without a Cloud Connection?
- Q3. Can QIDI Printers Use Third-Party Filament?
- Q4. Does Changing Nozzle Size Require a Firmware Modification?
- Q5. Can QIDI Studio Import STEP Files From CAD Software?
Рекомендуемые продукты